Conveyor belts for recycling
Conveyors in the recycling industry must be able to withstand rough handling and operate efficiently. Read all about conveyors for...
English
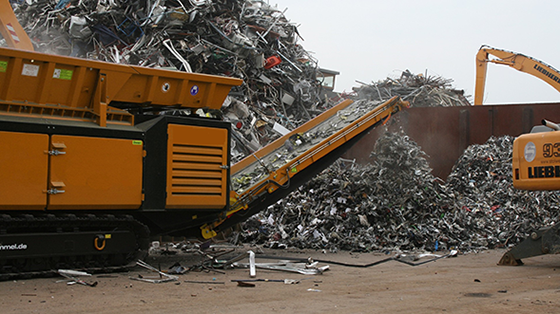
Conveyors in the recycling industry must be able to withstand rough handling and operate efficiently. Read all about conveyors for...
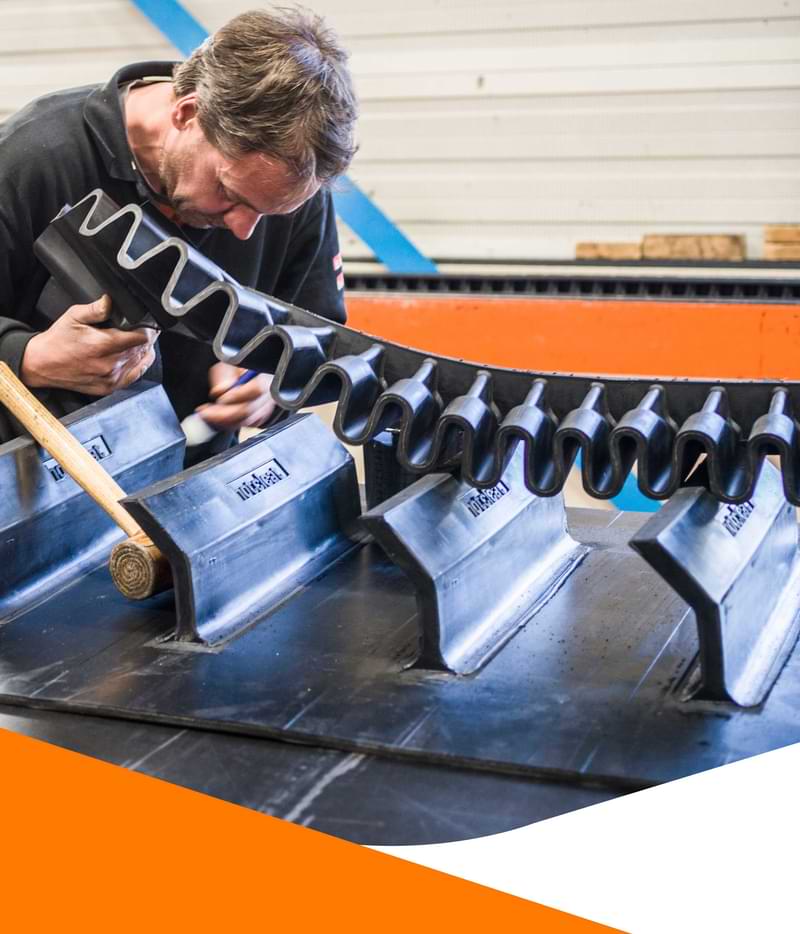
Discover high-quality conveyor belts with cleats for every industry. LBS offers durable cleated conveyor belts, hot vulcanised for...
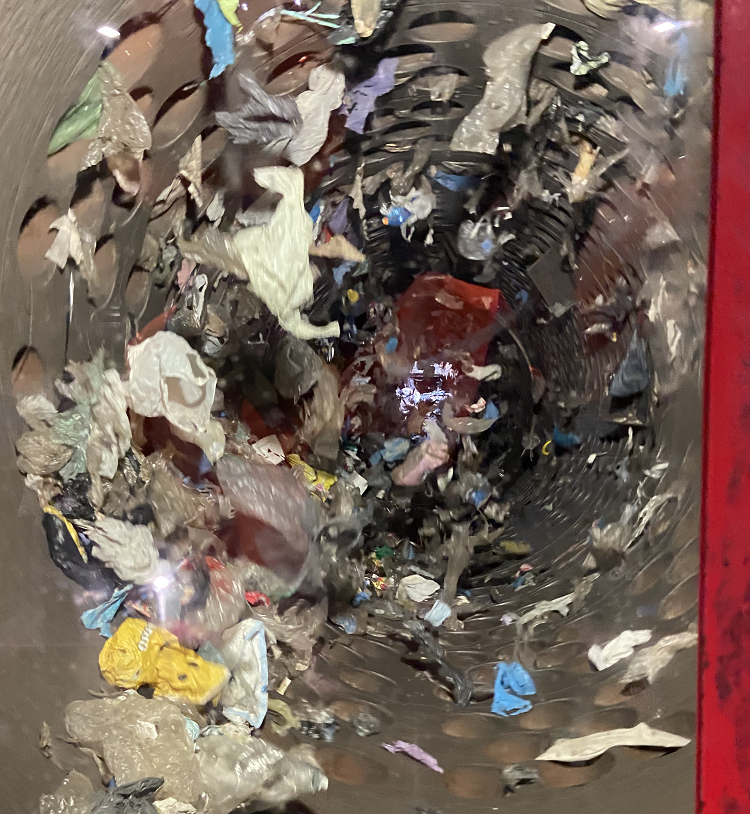
In drum screening machines, conveyor belts play a crucial role in increasing performance, improving throughput and optimising the...

Most synthetic conveyor belts meet the latest food safety standards for use in food processing machinery.
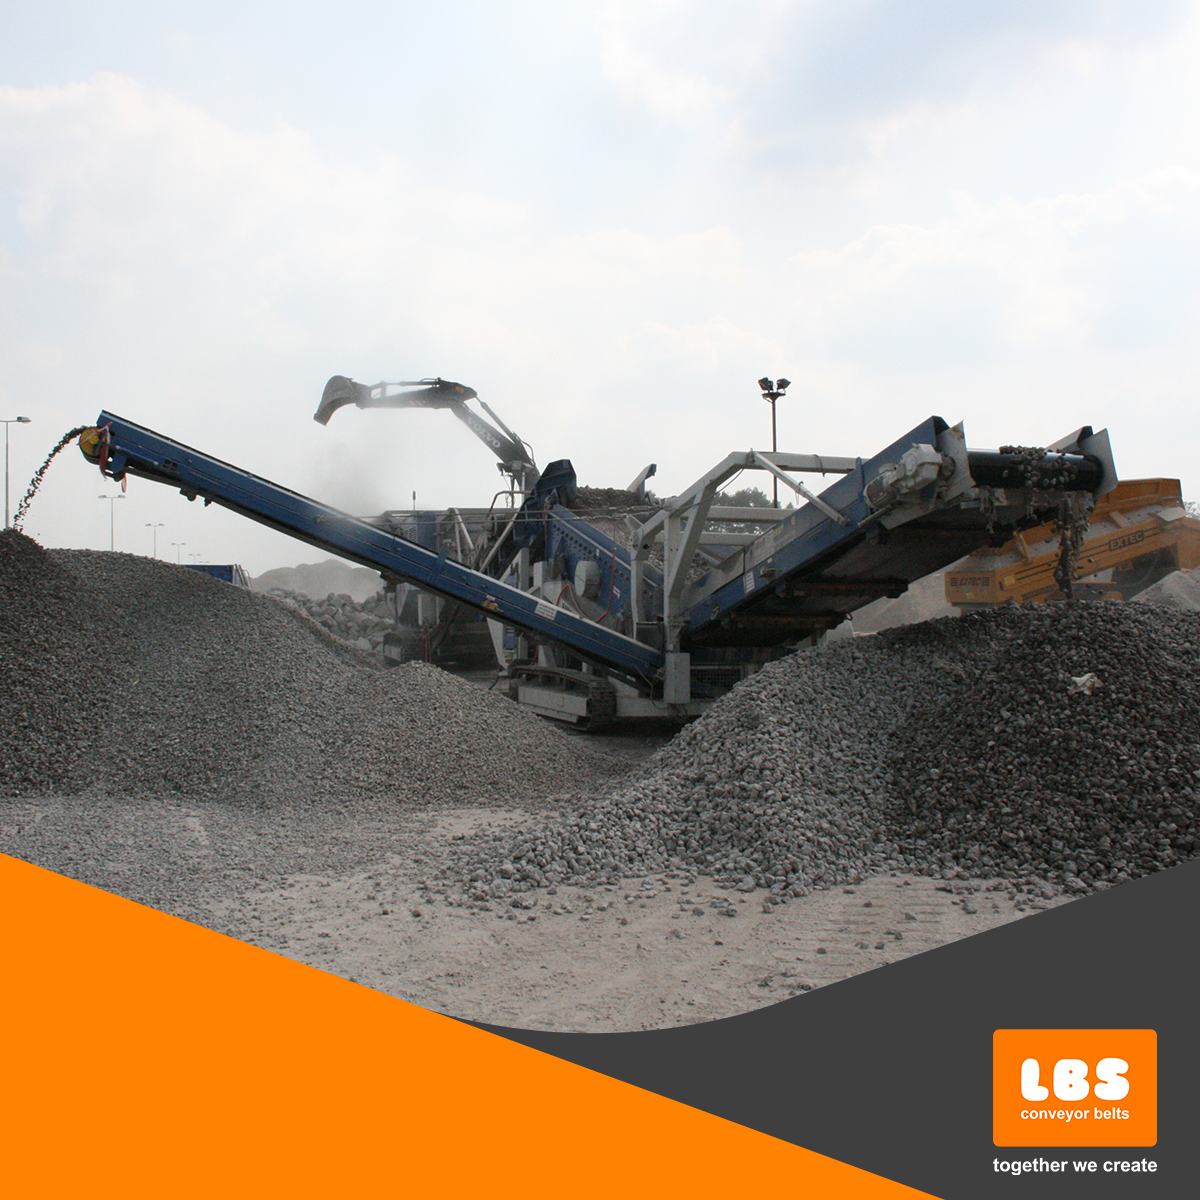
The ideal conveyor belt for rubble crushers in the recycling industry. What do you need to consider? You can read about that in...

ISO certified emphasizes identifying and improving processes to ensure the quality of products and services.

Invest in quality: Why cheap is often expensive with conveyor belts, read more about it in this blog.
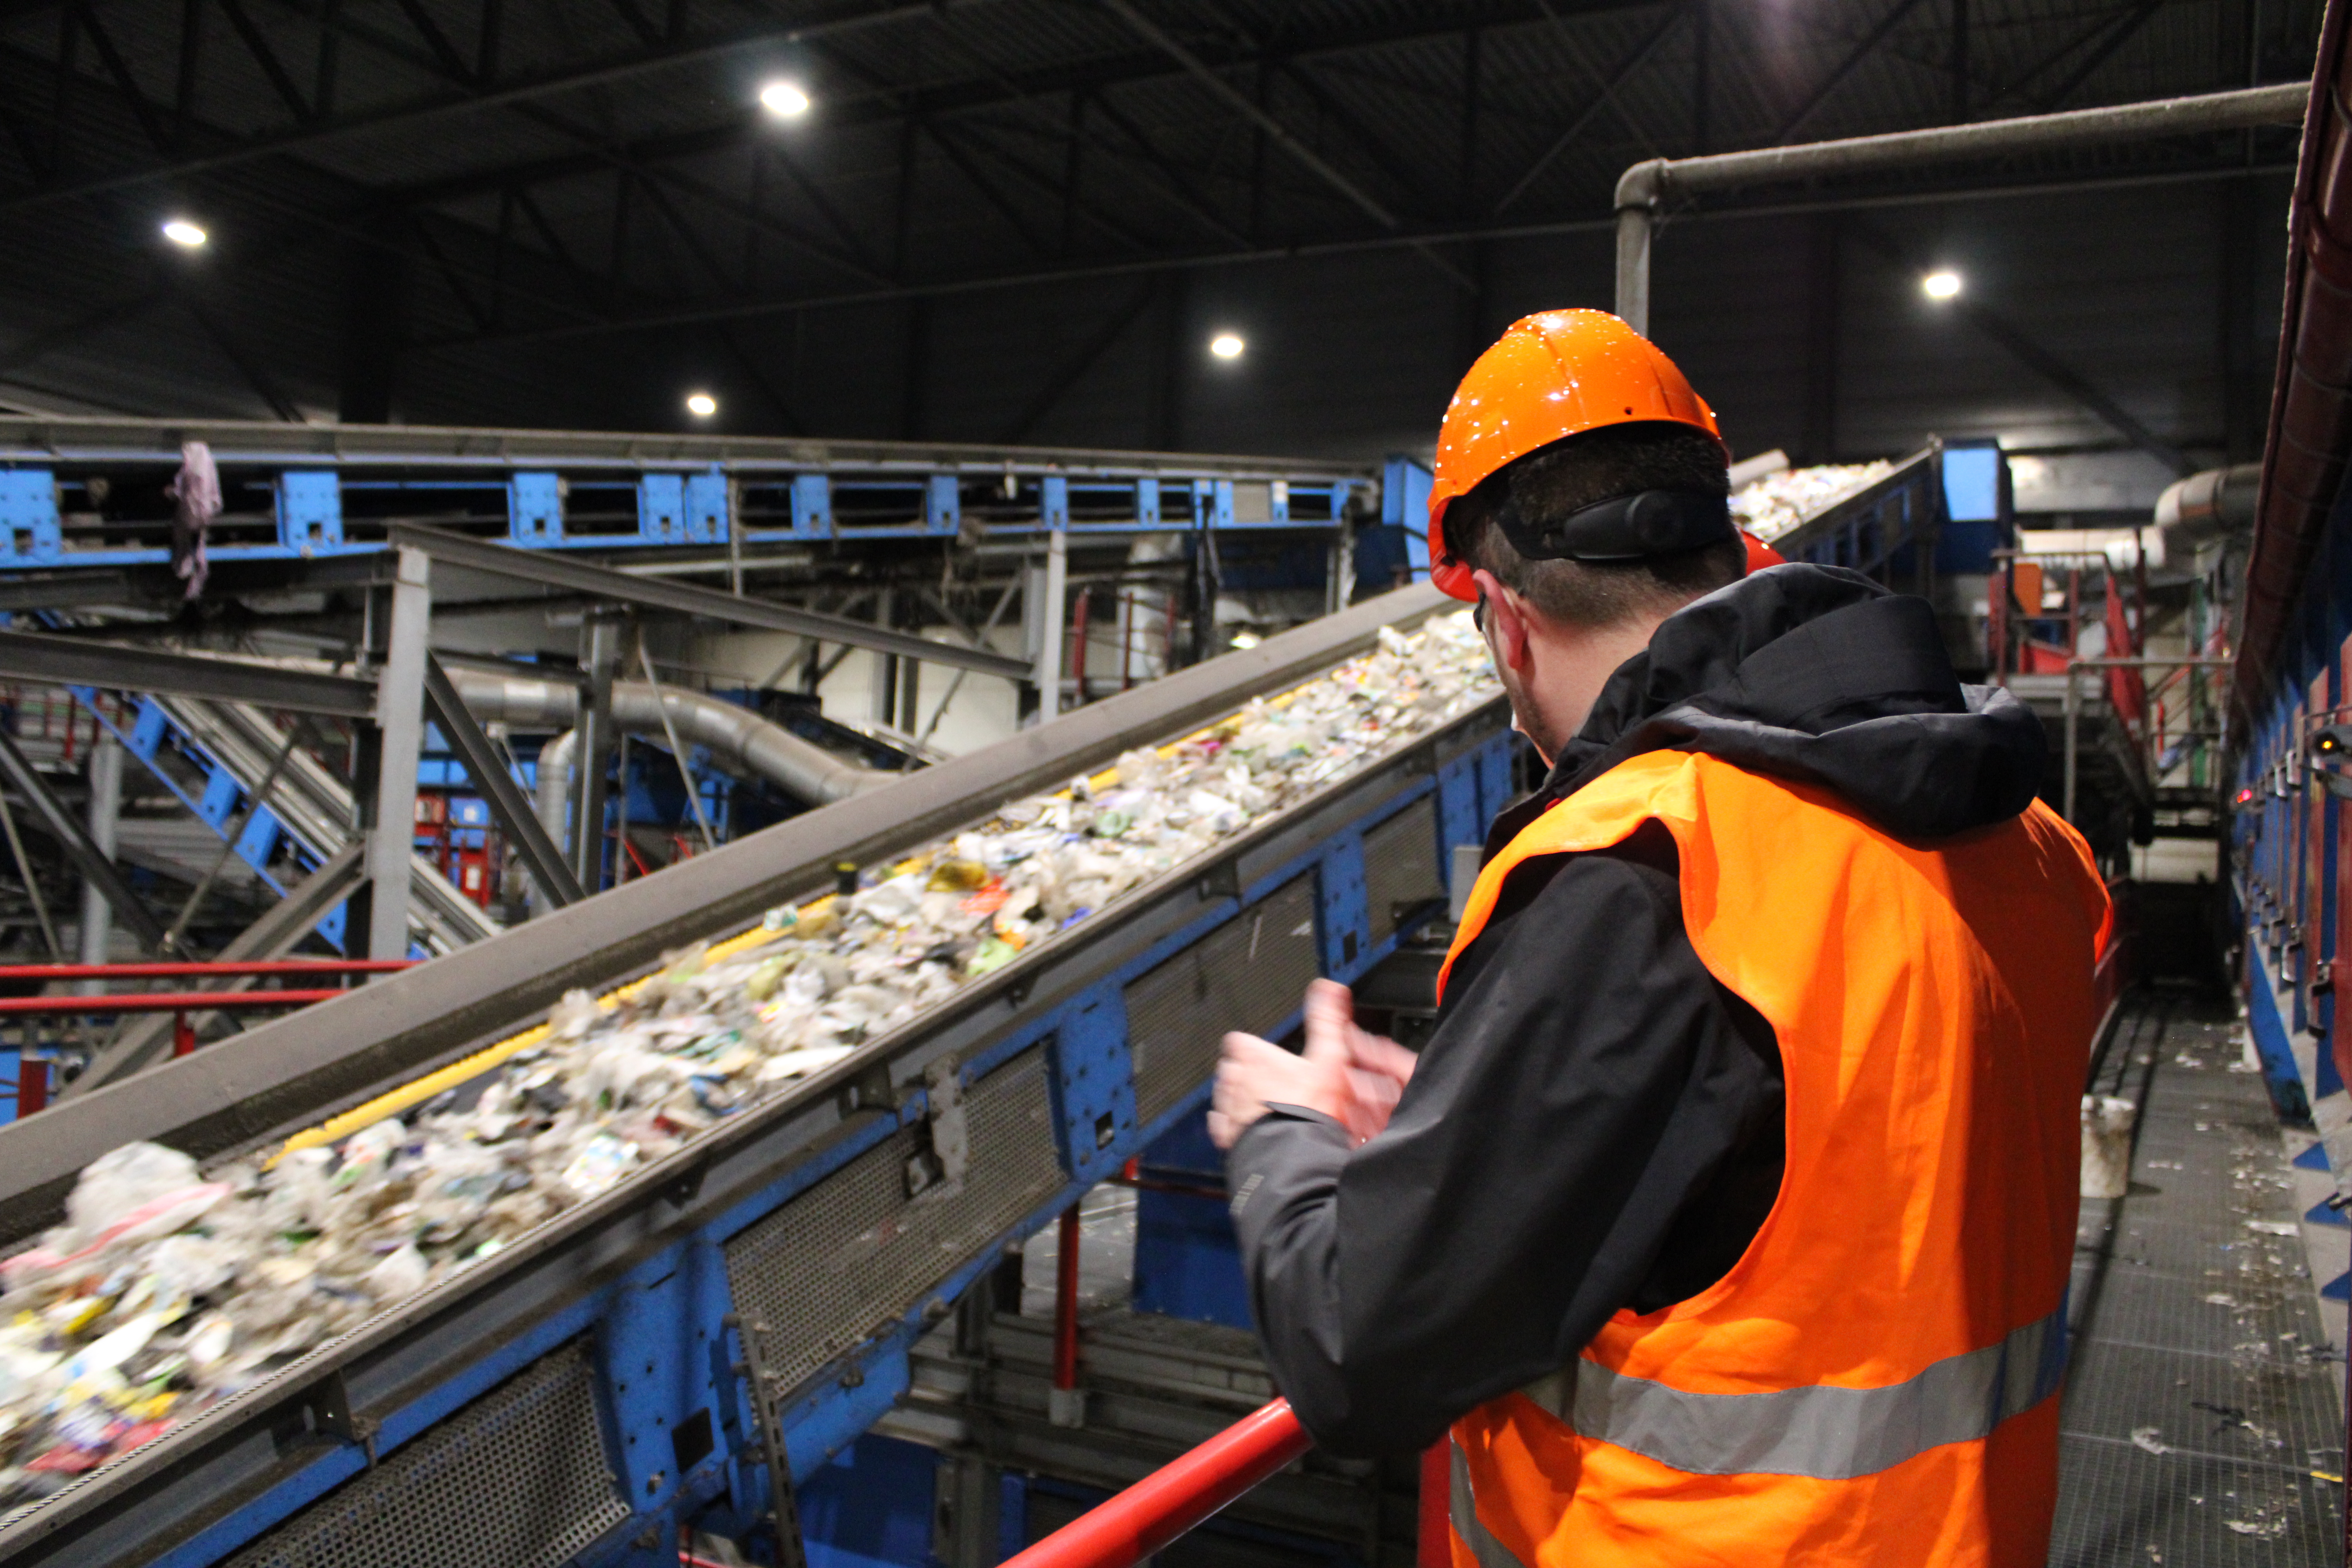
In this blog, we discuss five essential tips for maintaining your conveyor belt to keep it performing optimally and save you costs.
These profiles on synthetic conveyor belts are suitable for various applications because of their individual properties.

Boost capacity with sidewall conveyor belts at LBS. Our Hotwall technology and corrugated designs save space and increase...

Are you looking for the right steering belt for your conveyor belt? We provide guide ropes and strips for your conveyor belt that...
As of 1 June, management of LBS will be handed over to a younger generation. Jan Schaft and Eric Telgenkamp will be giving new...
