CONVEYOR BELTS IN A DRUM SCREENING MACHINE
In the world of modern industry, technology has proven time and again to be the driving force behind efficiency and innovation. One such technological gem used in numerous applications in different sectors is the drum sieving machine. While the drum screening machine is a remarkable invention in itself, conveyor belts play a crucial role in increasing performance, improving throughput and optimising the entire process. In this article, we dive deeper into the world of conveyor belts in a drum screening machine and discover why they are so revolutionary.
The basics: what is a drum screening machine?
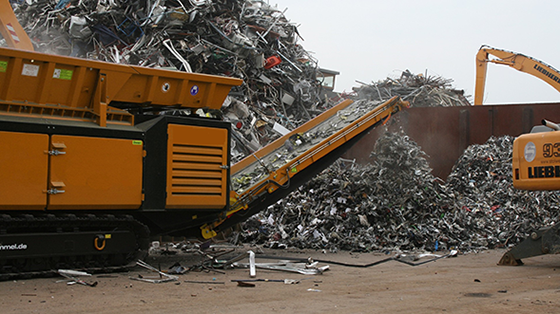
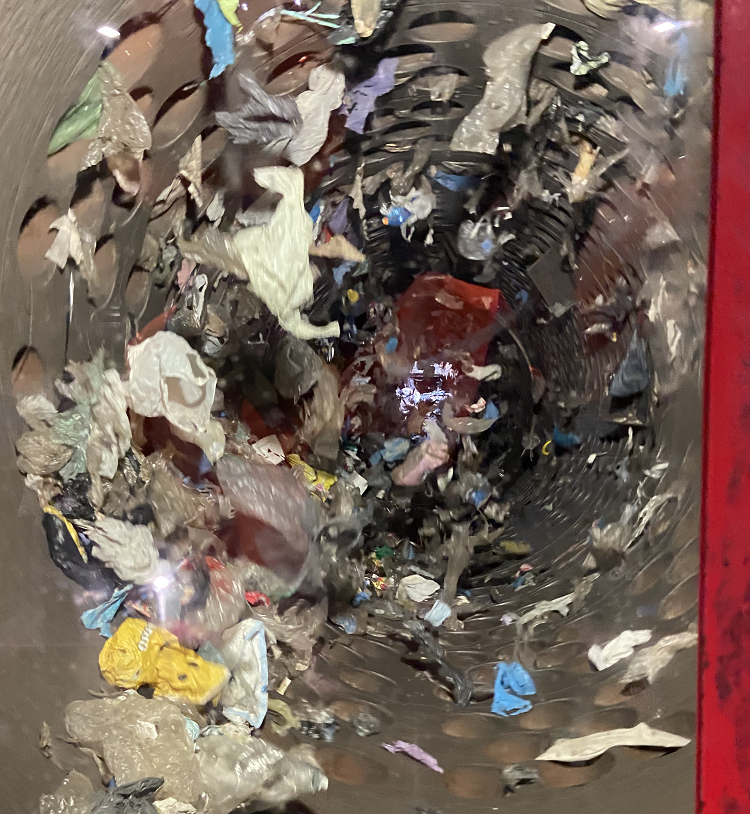
Before we explore the role of conveyors in a drum screening machine, let us first understand what exactly a drum screening machine is. A drum screening machine, also known as a drum sieve or sieve drum, is a device used to sort and separate materials such as soil, rubble, minerals and even compost according to their size. The device consists of a rotating drum with perforations of different sizes. Materials are fed into the drum and as the drum rotates, smaller particles are separated by the perforations, while larger particles are discharged at the top.
The power of conveyors:
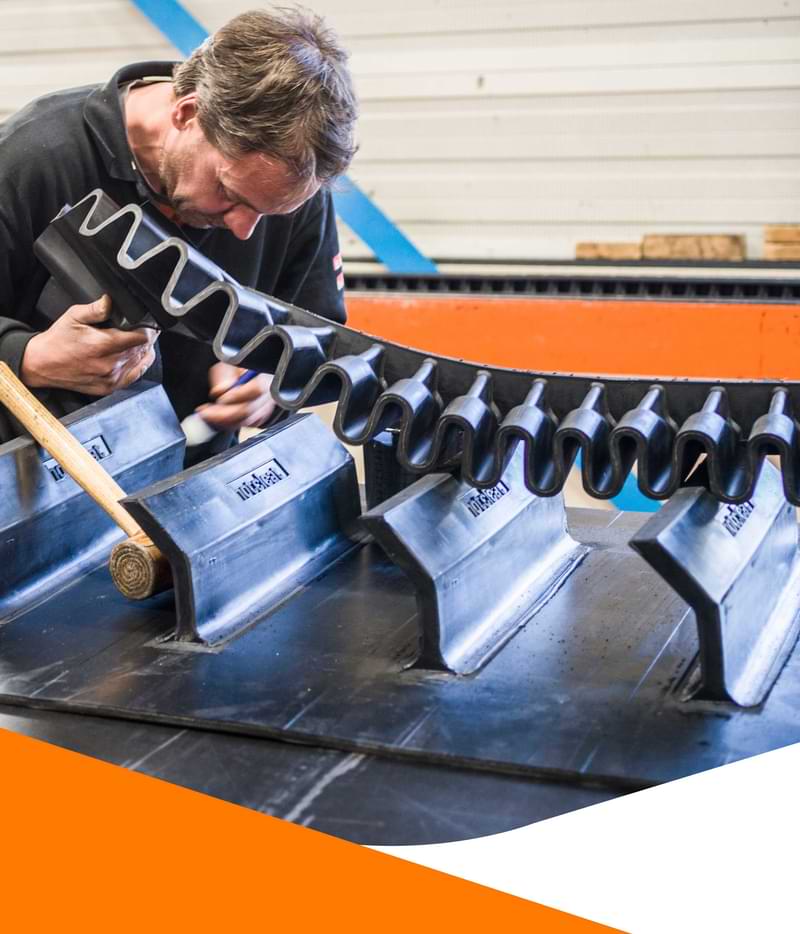
Conveyors form the backbone of a drum screening machine. They play a crucial role in moving materials through the screening process, and their design and performance directly affect the efficiency of the machine as a whole. Here are some of the ways conveyors make a difference:
-
Material feeding: Conveyors continuously feed material to the drum sieving machine, ensuring a steady supply of materials to be sieved. This prevents hiccups and ensures that the machine can run at full capacity.
-
Balanced distribution: The conveyors help distribute the incoming material evenly across the width of the drum. This prevents overloading on certain parts of the drum, extending the life of the machine.
-
Efficient separation: As the drum rotates, the conveyor belts push the material against the perforations. Smaller particles fall through the openings, while larger particles are discharged at the top. This process is facilitated by the constant movement of the conveyors.
-
Variable speed control: Modern drum screening machines often have conveyors with variable speed control. This allows operators to adjust the feed speed to the material to be sieved, resulting in better separation and optimisation of throughput.
-
Disposal of residual material: After sieving, a conveyor transports the separated material away from the drum, making room for new material. This continuous process minimises downtime and increases overall efficiency.
Conclusion: the future of efficiency
Conveyors form the backbone of a drum screening machine and are indispensable for the smooth running of the screening process. The combination of a rotating drum and moving conveyors makes it possible to sort and separate materials on a scale previously unthinkable. Thanks to continuous innovations in conveyor technology, drum screening machines are becoming increasingly powerful, accurate and efficient, making them an indispensable link in various industries, from construction to mining and waste management. With conveyors playing a crucial role in the process, the future of the drum screening machine remains full of promise for further progress and optimisation.
Do you have questions about this or other questions about conveyors? Contact us, our specialists are at your service.